Your component requirements.
Explore the workpiece materials, shapes and production tasks suited to this equipment.

- Inner and outer diameter with section and thickness
- Material, weight and inspection surfaces
- Fixture, contact and orientation requirements
- Changeover and onward handling
From loading to the next operation.

The process brings together workpiece loading, treatment and transfer to the next operation.
Equipment details.
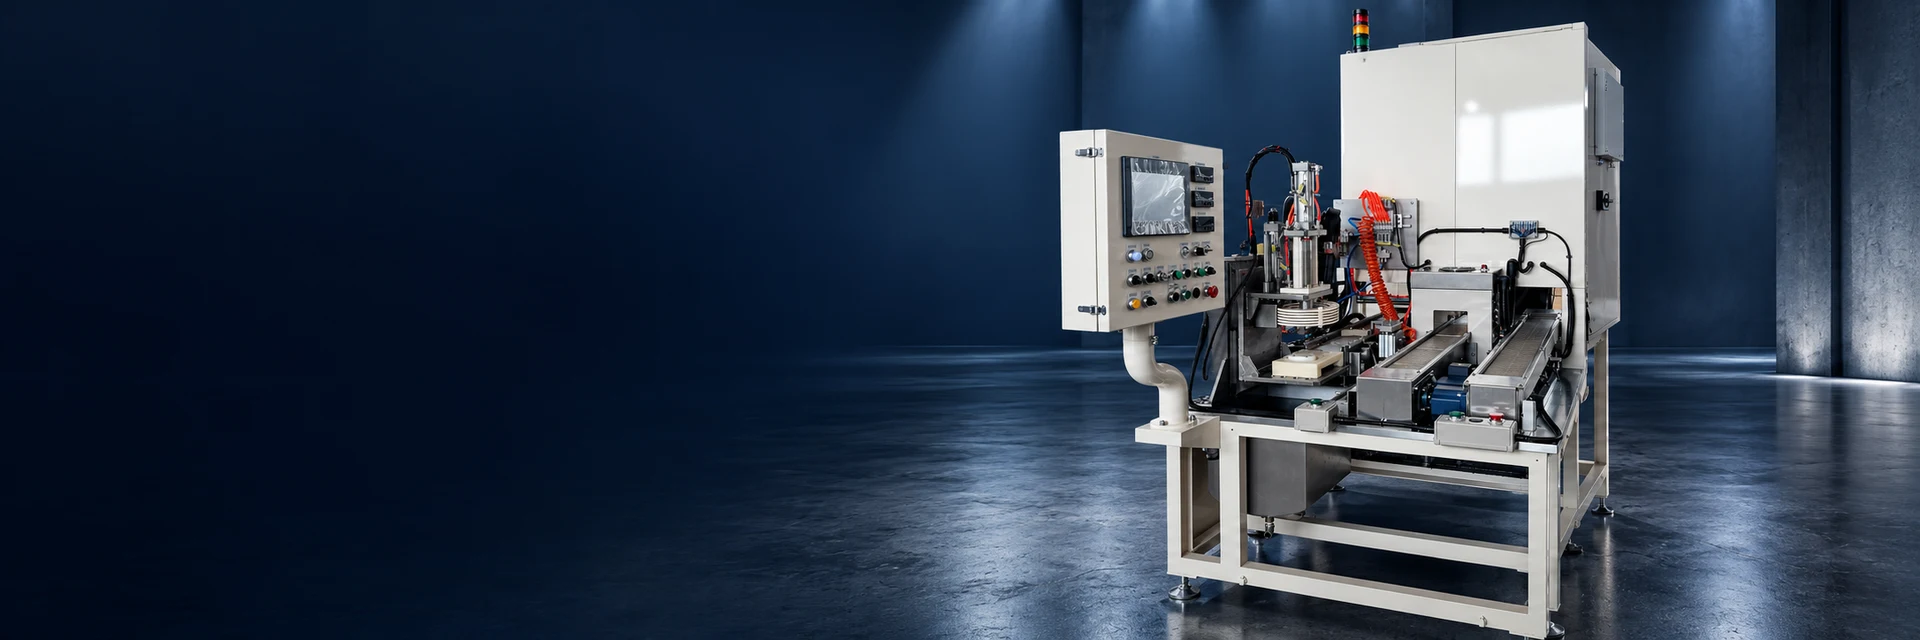
Ring-component positioning with an adjacent control panel.

Inspection around the ring geometry.
Inner diameter, outer diameter and section thickness guide the locating and magnetization arrangement. Material, weight and inspection surfaces complete the workpiece description.

Workpiece positioning and operator inspection.
Fixtures present the ring for magnetization and viewing. For several ring sizes, the loading arrangement and fixture changes are selected across the complete component range.

From inspection to the next operation.
Accepted and rejected part routes organize unloading. Where demagnetization is required, include the residual-field limit and measurement positions in the enquiry.
Your equipment
questions, answered.
Find answers about materials, part handling and inspection or cleaning processes.
Which materials are suitable for magnetic particle inspection?
Magnetic particle inspection is used for ferromagnetic components, including suitable steel and iron parts. Aluminium, copper and other non-ferromagnetic materials require a different inspection method.
Include the material grade and manufacturing condition with your enquiry.
What component information is needed for an MPI system?
Send drawings showing the complete part range, dimensions, weight, shoulders and end features. Mark the surfaces that need inspection and any restrictions on clamping or electrical contact.
For multiple part sizes, include the smallest and largest variants.
How are the magnetization settings selected?
The material, component shape and inspection procedure guide the current type, field direction and magnetization settings. Include the required inspection areas and acceptance criteria with the workpiece drawings.
The fixture and magnetization arrangement are selected together for the component.
How does operator inspection fit into automated MPI?
The equipment can coordinate loading, clamping, magnetization, particle application and transfer. An operator examines the fluorescent indications and determines the result using the inspection procedure.
Production output includes the time for workpiece handling and operator inspection.
Can the equipment use manual or mechanical loading?
Manual loading, mechanical handling and production-line connections can be considered for the component and required output. Part orientation, fixtures and transfer height guide the loading arrangement.
Include the incoming and outgoing part flow with your line layout.
What information is needed for demagnetization?
Include the residual-field limit, units, measurement method and measurement points. Component material, previous magnetization and the next operation help select the process and handling.
For a new part family, representative components help evaluate the demagnetization process.
What drawings are useful for shaft inspection?
Include shaft length, diameter changes, shoulders, end features, weight and inspection areas. Add the material grade, manufacturing condition and intended loading direction.
Drawings for the full shaft range help plan fixtures and changeover.
Can one system inspect several ring sizes?
A shared arrangement can be considered across the complete ring range. Inner and outer diameters, thickness, weight and inspection surfaces guide fixtures, magnetization and operator access.
Provide the smallest and largest ring drawings, along with any section changes.
Connect the details.
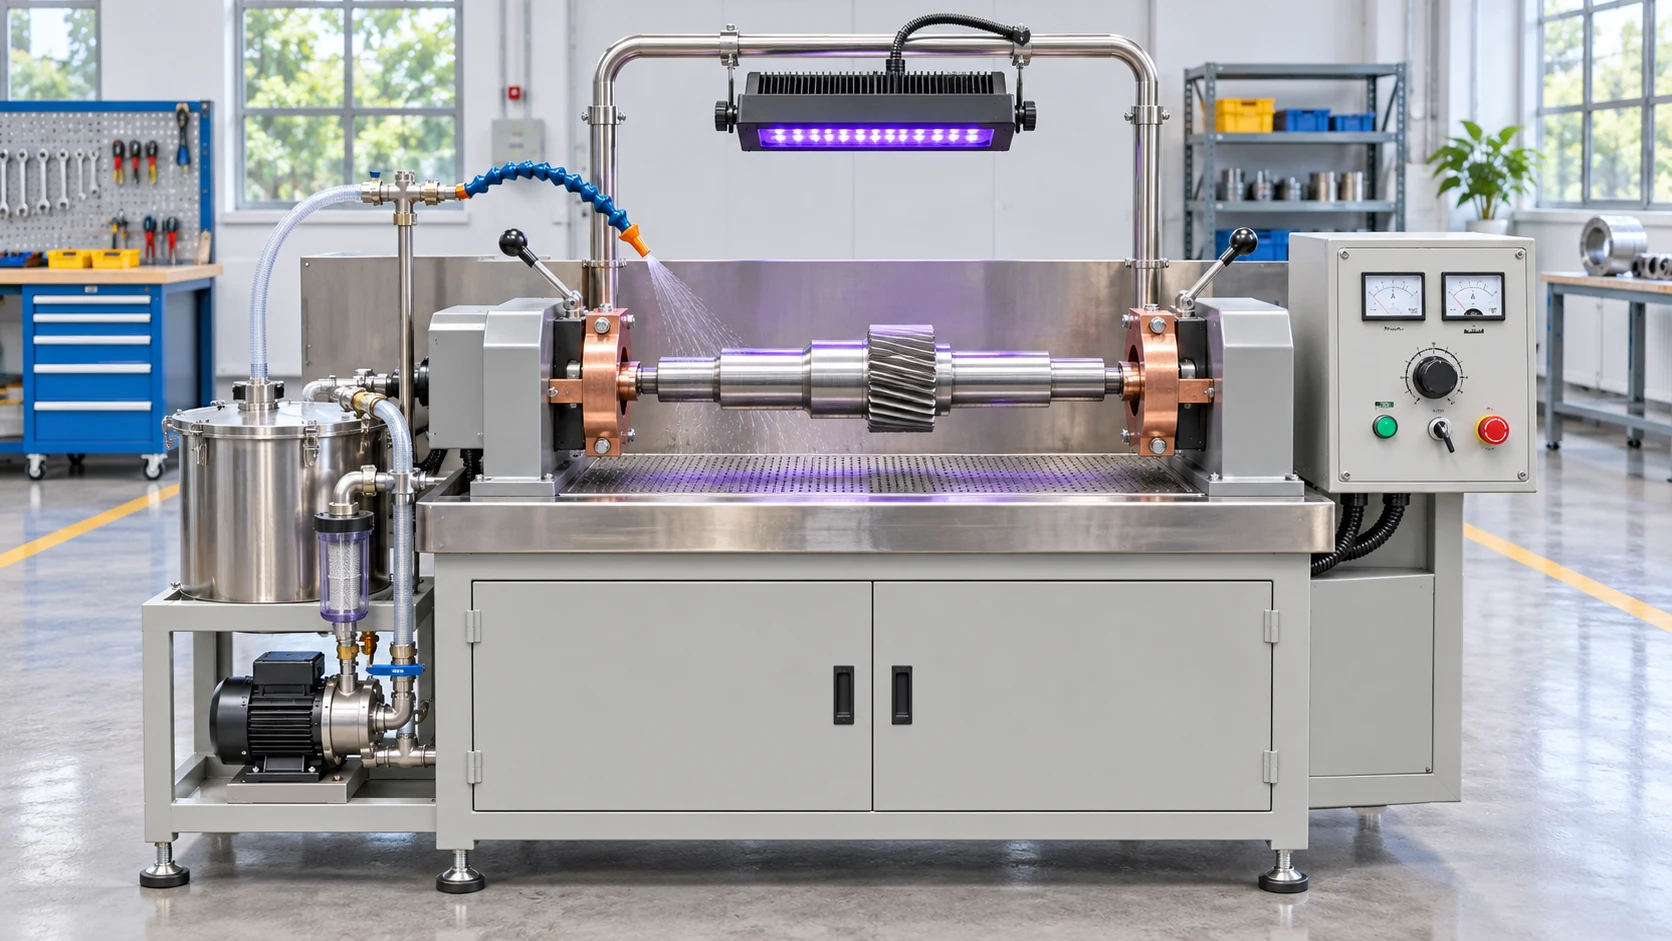
Magnetic particle inspection equipment
Plan fluorescent magnetic particle inspection for ferromagnetic shafts, rings and machined parts. Compare workpiece handling, magnetization and operator access.
Explore the application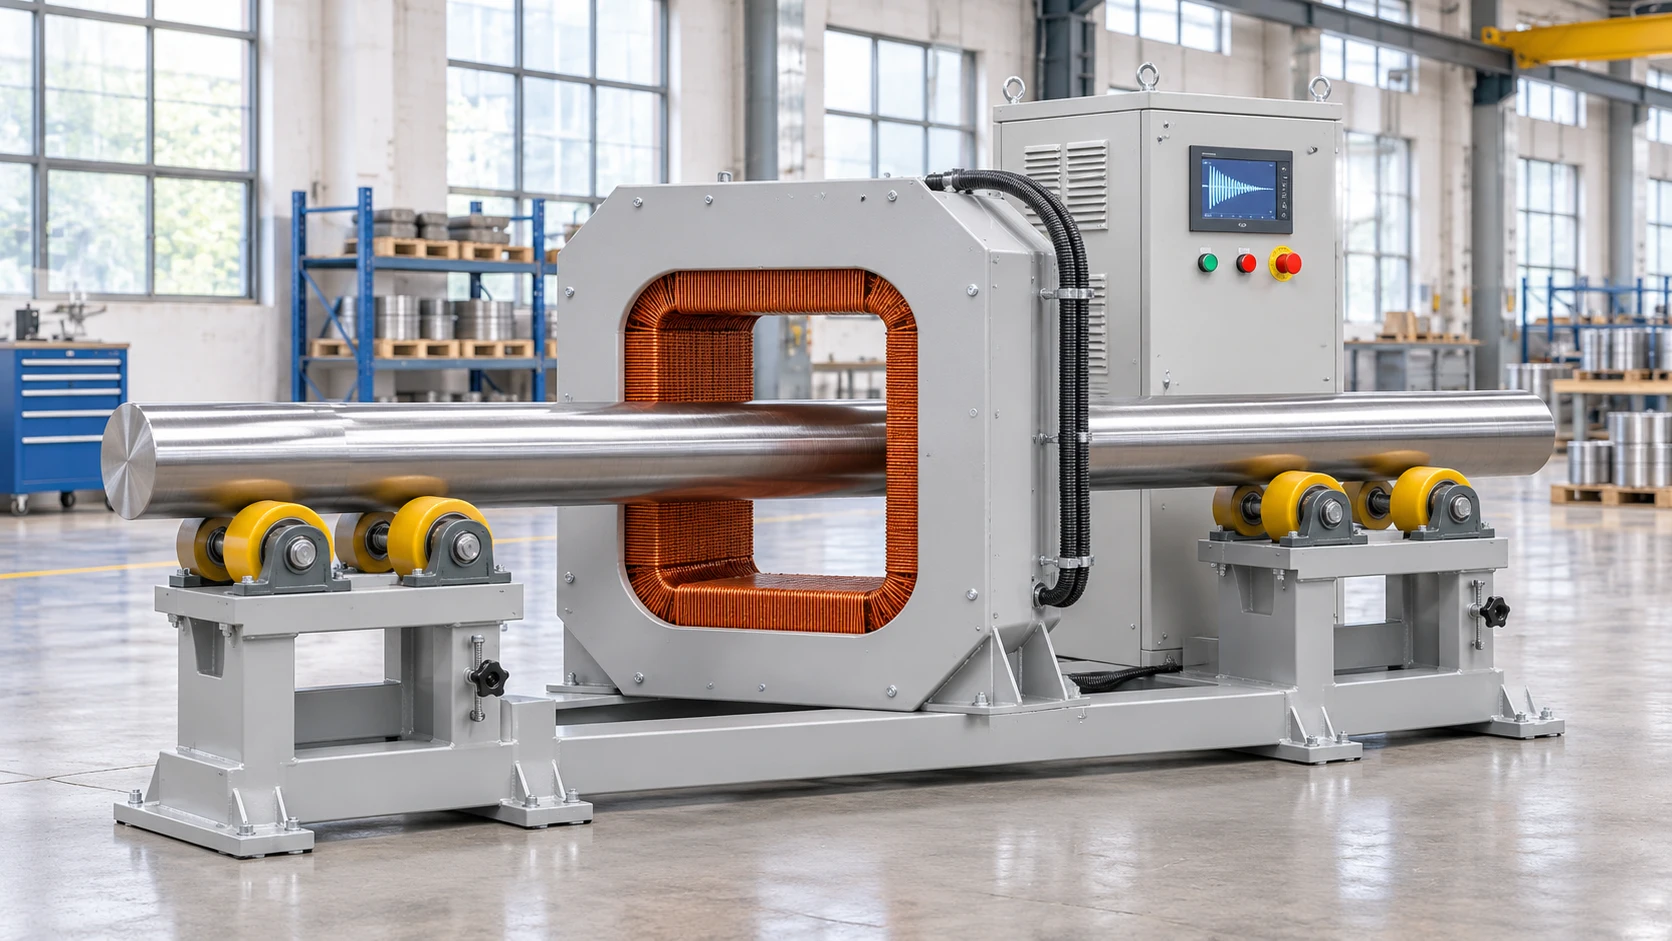
Industrial demagnetization
Evaluate demagnetization for ferromagnetic components after inspection or magnetizing operations. Define part handling, the residual-field limit and measurement points.
Explore the application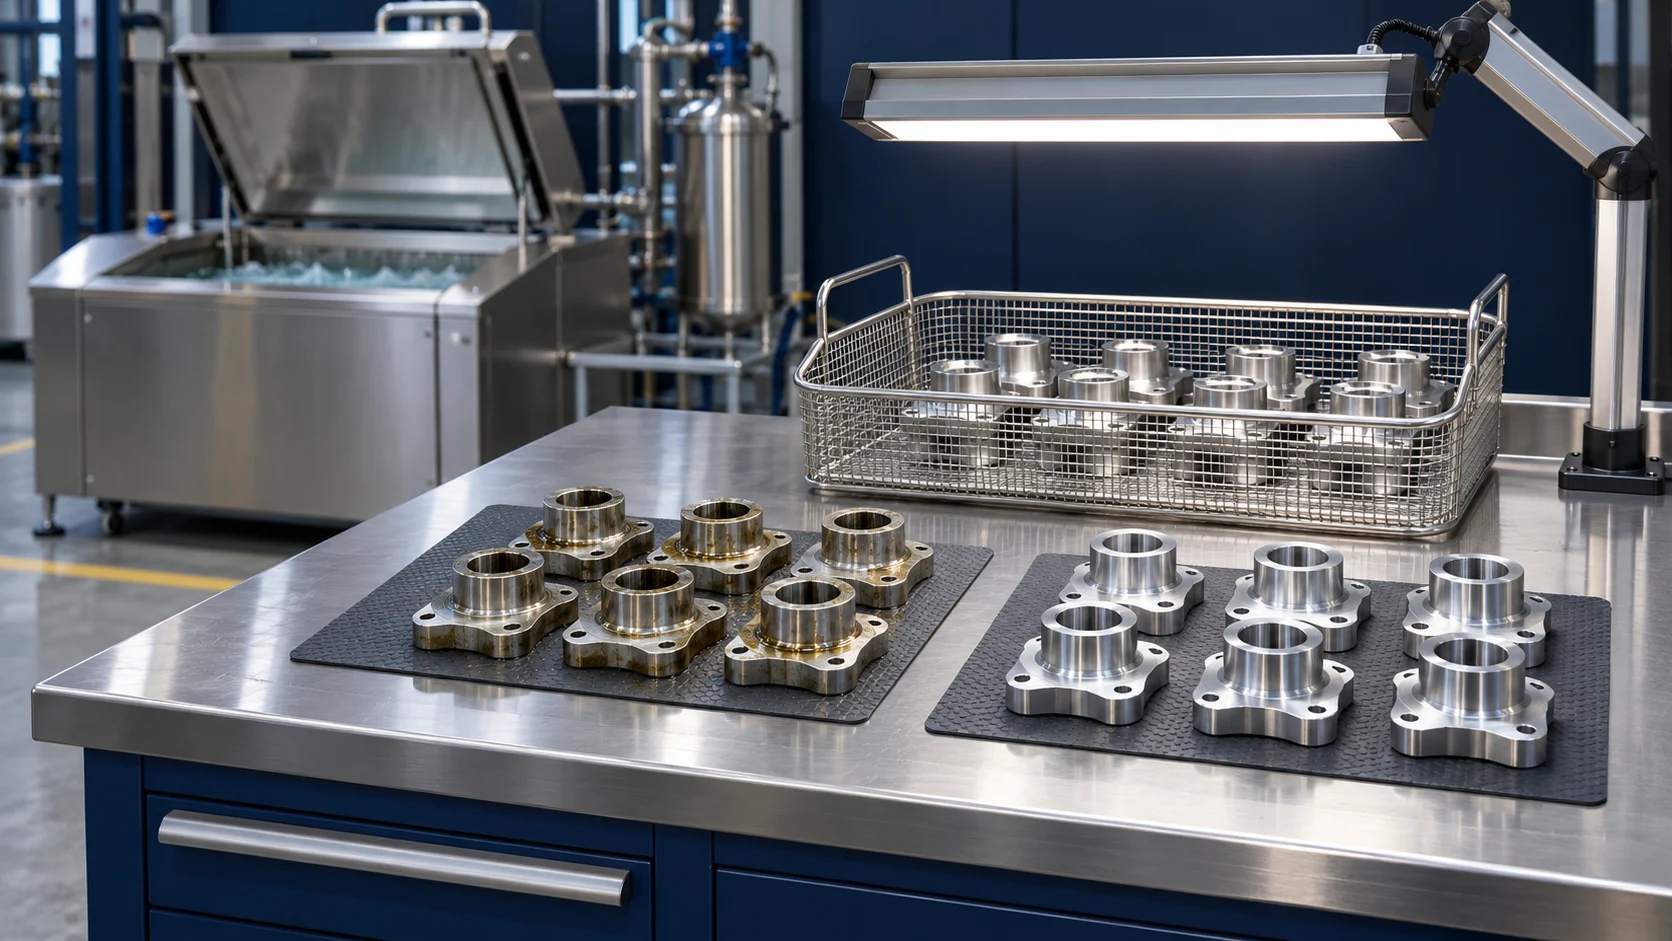
Sample testing for your parts.
Prepare representative components for a cleaning or magnetic particle inspection trial. Define incoming condition, test procedure and acceptance before comparing results.
Explore the application